Category: Iacdrive_blog

Power factor of a generator connected to national grid

Q: What should be the power factor of a generator connected to national grid in order to have maximum stability? Whether it should be high or low?

Steady State Stability:
1. National grid is like a infinite bus for an average size Generator. We can observe stable operation of generator within its capability limit for all ranges of power factor for infinite time , irrespective of power factor.
2. Observe the load cycle, The generators operate in overexcitation mode (lagging pf) during the day & during night ,when transmission lines generate enough reactive the same generators operate stable in underexcitation mode (leading pf).
3. Therefore as long as there is no instance of large disturbance, we can observe stable operation of generator within its capability limit for all ranges of power factor.

Transient Stability:
1. Depends upon the initial condition of the generator operation (see on Power vs Sin-delta plot)
2 The level of power thrown-off causing the disturbance & Equal area criterion of the energy balance & Inertia.
3 During transient/disturbance, the stability is ensured better if the angle delta (rotor angle or power angle) is small, meaning the amount of store energy in the rotating system is high. Theoretically this means delta angle =0 to have robust stability, but it is practically impossible to have power generation at that value.
4 In order to have maximum stability & power generation simultaneously , the value of rotor angle has to be non zero , on positive side. (negative means motor operation).
To Conclude : It means over-excited mode.(lagging pf ). Many colleges in discussion chain above have written near about 0.9 – 0.94 lagging . They are correct.
Frequency Inverter Direct Digital Control

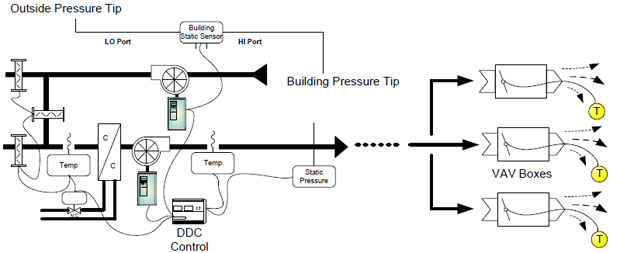
Modulating Supply & Return Fans are used as a means of providing proper variable air volume (VAV) control as well as building pressurization. Many such VAV systems are still largely pneumatic with static to the downstream boxes being maintained by inlet guide vanes. To provide increased energy savings and energy comfort, these systems can be easily converted to frequency inverter fan control of the supply and return fans and Direct Digital Control (DDC) to coordinate any increased energy saving strategies. Figure 1 shows such a system.

Frequency Inverter Direct Digital Control

To increase energy savings, the DDC controller can be programmed to reduce the flow from the return & supply fans for short periods of time. Coordinated with the building pressurization system, any temporary loss of space temperature may be avoided.

In Figure 1, the supply fan is controlled by the duct static pressure sensor, via the DDC, while the outside air and mixed air dampers are optimized to provide economizer control.. The return fan is modulated to stabilize building pressure at a slight positive. For simple supply and exhaust systems the building pressure and static pressure sensors may be connected directly to the frequency inverter with an internal PID controller.

Typical Energy Savings are realized from converting pneumatic (or electromechanical) control to DDC control with frequency inverter in the following ways:

  • Locking inlet guide valves mechanically open to allow the frequency inverter to fully modulate the fans.
  • Free cooling by accurately modulating the economizer dampers and sequencing the mechanical equipment.
  • Controlling static and resetting the static pressure during short periods of time.
  • Accurate building pressurization.
  • Implementing other energy saving measures which include supply air reset, and night purge routines.

CONTROL CONSIDERATIONS

  • Placement of the indoor static pressure sensor is important as it should provide a stable signal. Entrances, dock, and other areas where large , sudden static pressure changes may occur should be avoided.
  • The outside reference static tip should be shielded from wind and rain.
  • When the exhaust fan is frequency inverter controlled, consider a 2-position air damper to prevent the outside air from entering the building (infiltration) when the exhaust fan is off or a very low speeds.
  • For simple VAV systems, consider using frequency inverters with built in PID controls such as the Iacdrive frequency inverters.. This minimizes hardware and installation costs. Static sensors provide a 0-10vdc control signal directly to the frequency inverter.
  • Duct mounted static pressure sensor should be mounted 2/3 of the distance of the distribution system.

variable frequency drive

Current transformer selection

When you want to select current transformer with appropriate rated power for your power system, you need to consider that value of rated power of selected current transformer should be higher from sum of values of load and Joules’ losses which are a consequence of flow current through conductors which connect current transformer with relay.

So, if you have a long distance between current transformer and relay, then you need to consider one of two following manners for solving this problem:
1. replacing existing current transformer with current transformer with higher power,
2. replacing existing conductors with conductors with lower cross-section.

This solution is a consequence of necessity for reducing of Joules’ losses which are a consequence of flow current through conductors which connect current transformer with relay. If you have conductors whose value of rated current is 5A, you will have Joules’ losses P=R*I^2=R*5^2=25*R. Otherwise, if you have conductors whose value of rated current is 1A, you will have Joules’ losses P=R*I^2=R*1^2=R.
On this way, Joules’ losses in your selected conductors will be reduced 25 times and selected current transformer will be unloaded by reducing additional load.

Rotary Tube Furnace Efficiency

There are many factors that govern the performance of rotary tube furnaces. A direct fired rotary unit has a potential for much higher thermal efficiency due to the direct contact of the hot gases with the material in process. Cement kilns are the most common large scale unit operation with direct fired units. Any articles you find on this will be helpful. Thermal efficiency can be estimated by dividing the inlet temperature minus the outlet temperature by the inlet temperature minus the ambient temperature in absolute scales either Rankine or Kelvin. Then there is the issue of co-current versus counter-current firing and heat recovery from the hot material and the exit gas for which standard designs are available. Indirect fired rotary kilns have heat transfer limitations due to the thickness and alloys needed for high temperature calcination >500 C. There is no simple way to measure the equivalent of the inlet and outlet temperatures on a direct fired unit. There are simply exit gas temperatures from each zone and an approximate shell temperature on the hot side of the shell which is lower than the zone exit gas temp. These are useful for control purposes and consistent operation. The higher the temperature the material requires to achieve conversion the higher the shell side fired temperature has to be to provide the delta T necessary to drive heat through the shell into the material zone.

Some materials further limit heat transfer by adhering to the inside of the shell and acting as an insulator! This requires trial and error application of “knockers” at the ends of the shell or sometimes internally secured chains that bang around and knock the adhering material loose. This is a potential nightmare as the learning curve to install chains so that the securing lugs and the chains themselves will stay attached for acceptably long service before failing and ending up in the take off conveying equipment with usual breakage and downtime is an uncertain one. From Perry’s one can find thermal efficiencies for indirect fired rotary’s given as less than 35%. The bed fill can be 10-30% depending on the heat demand of the material and the heat transfer limitations. You will want to have real time gas usage metering on the burners so that you know the theoretical energy input. From that you can subtract the theoretical heat needed to complete your reaction and compare that to the input to see how efficiently you have used the energy input.

The few large high temperature direct fired rotary kilns I have seen had view ports for measuring the local wall temperatures by optical pyrometer. It can be a challenge to get a protected thermocouple sheath down into the moving bed for an actual bed temperature and even just to hang it in the gas streams at the outlet or inlet area. See if you can contact cement kiln suppliers for some configurations of temperature sensing elements for your application. Bed fill effects on heat transfer are related to several parameters. Above ~500 C gas and refractory liner temperatures, the main heat transfer mode will be radiative as far as the surface of the bed material. Within the bed it will be conduction and some convection at the surface. A thin bed will reach max. temperature in shorter time, but this reduces through put for a given gas temperature. If you increase bed fill to increase production you will have to increase the firing temperature and the outlet temperature will probably increase lowering your thermal efficiency. This becomes a trade off between production rate and energy efficiency. Countercurrent firing usually maintains the highest driving force for heat transfer along the bed and gives the highest temperature of the bed just before exit of the bed material.

Perry’s may have a useful section on direct fired rotary kilns and lime or cement manufacturing references may help you as well. Please make sure lead emissions to air are properly captured

Calculate Capacitors Power

In general, to calculate the necessary Power of Capacitors, we can use the following formula:

Qc = P ( tgφ1 – tgφ2 )

where :
– Qc : the Power of Capacitors.
– P : the total Power of Loads that are running during normal working.
– tgφ1 : the tangent of φ1 ( the angel between current & voltage before compensation )
– tgφ2 : the tangent of φ2 ( the angel between current & voltage after compensation )

In all cases, we should take into consideration the following points :
1- It will be better to oversize the calculated Qc by ” 10 to 15% “.

2- Be careful when compensate the PF of a Motor to avoid the Over-excitation case, but we can verify it by using the following formula : Qc (motor) = 2 x P (1 – Cos φ ), where :
– P : the Motor’s Power.
– Cos φ : the PF of the motor before compensation.

3- After calculation of Qc, the choosing of Capacitors type will be done according to the Harmonic Distortion percentage. Noting that in some case where the Harmonic Distortion percentage is high, we should use ” Detuned Reactors ” with Capacitors, and when this percentage is too high, we can’t install the Capacitors before minimizing or eliminating the harmonics that their percentages are too high.

Resistance to ground

Resistance to ground is greatly influenced by the ambient conditions and the state of the motor when tested.

Factors Affecting Insulation Measurement:
First, it is important to understand that we are measuring a motor circuit. We are connecting our test instrument at a point where we can measure the majority of the de-energized circuit. As such, we do not necessarily know where an insulation anomaly is located when identified. We also have the motor circuit potentially exposed to differing environments. Ambient temperature and humidity can have a significant effect on any insulation measurements. When a motor circuit’s insulation is tested is also a major variable. Testing a motor circuit immediately after shut down will most likely yield good results. This is because the motor is warm and dry. Testing a motor after it has been shut down for a while may indicate insulation problems, but if the motor is allowed to reach ambient temperature, the insulation integrity may appear normal. This is because while cooling, particularly in somewhat humid conditions, moisture (condensation) will accumulate within the motor and lessen ground resistance. Is this a problem? Yes, particularly if starting from a partially cooled state. Most motor failures occur during starting. This is when the insulation is exposed to the most stresses. If your motors are only down for a few hours at a time, then this is when insulation testing should be conducted.

When conducting insulation testing, the most important consideration is consistency. Always test at the same location, use the same test voltage, perform the test for the same amount of time, and use the same test instrument. It is also important to note the motor temperature, ambient temperature, and relative humidity. It is also helpful to compare like motors and the motors that are operating within the same environment.

Insulation testing is somewhat ambiguous. Although there are reference standards, they cannot be rigidly followed because they do not factor in all of the potential variables that may be encountered. Temperature is the biggest variable. Temperature of the motor and the ambient temperature are of primary concern. One method to help negate the influence of temperature is performance of a “Timed Resistance Test.” This testing is comprised of “Dielectric Absorption,” “Polarization Index,” and “Step Voltage” testing. Dielectric Absorption is a 1 minute test. The resultant values at 30 seconds and 1 minute are logged and the ratio of the 30 second value divided into the 1 minute value, is a relative indicator of insulation integrity. A polarization index is a 10 minute test with the resultant ratio derived from the 1 minute value divided into the 10 minute value.

So, if ground resistance is low after prolonged shutdown and it is at ambient conditions, then you probably have an insulation issue. Conditioning of the insulation may be required. A motor shop can perform a “Clean, Dip and Bake.” process which will prolong the motor longevity. If the motor is several years old you may want to HiPot the insulation but if you are not using one of the newer units that automatically shut down upon a jump in current, you may cause insulation failure and that would necessitate a rewind.

Generator reactive power

After the generator connected to grid, the generator will be more stable than before connected to grid, because in this situation the frequency and voltage are fixed and controlled by the grid, not the independent generators. How much active and reactive power you can contribute to the grid depends on the grid requirement, such as when the grid shorts of active power, the frequency of the grid will drop, and then the grid will ask you or other generators to contribute more active power, and if short of reactive power, voltage will drop, then you could be asked to contribute more reactive power, and vice versa, which depend on the balance of power which is generated from generators and consumed by the users.

From generator side, the less reactive power, the better, as this power increase the VA and then the current to increase the losses on the transmission line which will be carried by the plant. But from grid side, as not too many equipment can generate the reactive power, the more contribution of the reactive power, the better.

At the full load operation of generator, the maximum contribution of reactive power should depend on the PF of the generator at full load (manufacturer provided for each generator). If your PF is too low and it could affect your active power transfers to the grid and will be punished by the grid. At the not full load situation of the generator, the PF could not be decided by the generator, if the grid does not need too much active power from you, but needs more reactive power and asks you to contribute more, PF could be more than 1 at the moment, but never over the Max reactive power calculated from full load.

Solar power

On a purely theoretical level and ignoring interrelated economics and energy usage, it makes sense to charge EVs during the day – though never in non-distributed environments, IMO.

In reality, and the reality for likely the rest of my life, it makes more economic and particulate emissions sense to distribute solar power during the day to decrease, and ultimately decommission, fossil fuel sources used for peak demand supply that occurs during the day.

Thus, using solar output distributed to offset the dirtiest, most expensive and most distribution grid loading power enhances and optimizes the value and worth of that solar generated power – both economically and ecologically. Attempting, therefore, to do all of ones’ EV charging off peak is the optimal solution until the mix of energy sources changes dramatically – likely a 20 plus year process even in the most environmentally friendly “energy generation mix” regions of the world. Even if one charges during “peak”, it is better to simply charge from the grid as the distributed energy is allowed to go to areas of peak demand. Again, for at least my lifetime, I don’t project a more optimal use of that generation even assuming the archaic state of most “grids” persist.

Right now, even for a 1 story commercial building, solar cannot supply the energy needs used in the office, much less a manufacturing facility. In fact, it can normally only supply 1/3 or less for the most energy and resource intensive commercial environment in a UV intense region (and that is quite an optimistic calculation, more likely 1/5th). Once you get to two or more stories on the building, one is not even close. On a modest tower with a tower parking garage, the footprint is likely to small to even generate the needs on a theoretical basis. Distributing the energy to location of greatest needs will allow us to dial down and decommission peak sources, which again are the dirtiest and most wasteful.

At some point, we will hit a new equilibrium where the energy generation mix is much cleaner, solar generation specifically is much more efficient, and peak power generation is handled more efficiently and ecologically cleaner. I still believe, however, that distributed power is better than “off grid” type of scenarios as it allows the energy to go where it is being demanded at the moment, decreasing the need for redundant sourcing. And, even in the cleanest energy generation mix, redundancy means building more of something and is by definition more energy wasteful and ecologically wasteful than a scenario where the redundancy buffer that is required is lesser.

Much of this type of debate reminds me of the consumer sort recycle versus the destination sort recycle debate. Even with the advances in trash collection and recycling processes, 20 years later we are suboptimizing the recycling process. Much of the reason for that is the “style” statement, making people feel like they are contributing by sorting themselves. It may make some people “feel” better by imagining “independent” off grid or semi off grid solutions. In reality, however, we live in an interconnected world where “sharing” or distributing solutions to leverage scale and minimize redundancies is far more advantageous, economic, and a faster route to a solution to both particulate emissions issues and energy independence for groups of people.

Cleaning solvent for motor windings

Usually, the dry ice approach is the best bet because it leaves no real residue from the cleaning material. If the insulation is “fluffing”, the likely problem is that the air pressure used to move the dry ice particles is too high.

A second alternative that can be used is “corn cob blasting”. The media is reusable, biodegradable particles of corn husks. Again, a relatively low pressure air stream is required. It WILL damage the insulation if the pressure is too high, just as in the dry ice case.

Most solvents will aggressively attack the insulation systems used for windings: this is specifically true for the larger machines where mica tapes are coated / filled with a resinous material (vacuum pressure impregnation). However, it is equally true for smaller machines where the primary insulation is at the strand level and is essentially a varnish or enamel coating on the wire. If you’re worried about how the solvent will affect the insulation system, get in touch with the motor supplier for their suggested approach.

If a solvent-based cleaner must be used, it should be applied sparingly – BY HAND – on the areas to be cleaned to break up the oily / greasy contaminant and then rewashed with some other (non-solvent) approach to clean away any solvent residue. This also will require a “dry out” of the equipment after the second washing. This three-stage approach tends to minimize damage done by solvent that may be left behind to “eat away” at the varnishes, enamels, and resins comprising the insulation system.

One last thing – pretty much ALL solvents are going to be designated as hazardous materials in most regions, due to health concerns. Therefore it is more a case of “pick your poison”!

Negative Impact of Accelerated Depreciation on the Indian Economy

For argument sake or as an illustration, if we assume that 1 MW solar will generate 1.6 Mkwh and rs. 1.2/kwh is rebate for AD taken by the investor = 16 x 1.2 = Rs. 19.2 lakhs/year

[Now, Adani and Tata Power have been negotiating the firm Contract PPA to get more, like wise biomass people who based their PPA on LCOE, but, are asking more money from Government, hence, Solar PV developers may also follow the same route after few years, wherein this rebate of AD given will not have any meaning!!]

Total rebate given = 19.2/year x 25 years = Rs. 480 lakhs = Rs. 4.8 Crore (that too year wise depreciated / devaluated rupee value, which has no meaning !)

But, the tax saved is = 80% of investment = 0.8 x 10 cr = 8 Crore, upfront, right in the first year, which is great value, which government would have used as Equity to develop many more MWs.

Is this POLICY of providing 80% Accelerated Depreciation correct by any standards and why Finance Secretaries or policy makers can’t take note and issue corrective measure for INDIA FIRST Culture??

MNRE, in its Draft policy has proposed 20 to 40% Viability Gap Funding, which will further worsen the LOSS to the government !!

If Mahagenco (with 50% subsidy) goes ahead with the proposed business model, then, how and why State and hence Central government has to take the burden due to such errant policies??
We must put an end to the Scrupulous Project Development, which avails the Capital Subsidy (or Viability Gap Funding) and the Accelerated Depreciation and then the Promoters Sell the Project to a prospective buyer, who in turn approaches the Government for the Tariff hike in the 25 years tenure (please note the Politics dynamics or change of administrative set up will hamper the sustainability), thus, the nation is a great loser

Policies and the enabling tax advantages to few promoters (who claimed Capital Subsidy without creating good quality asset or with NON functional biomass power plants) have made a big dent on Indian Economy without any good results esp in Renewable energy sector.

Government or its administration through such policy (without checks or being accountable) transferred the Public Property to the Private Companies in the Form of Renewable Energy Generation through Capital Subsidy (or Viability Gap Funding) coupled with Accelerated Depreciation along with Low cost Debt fund to these Corporate companies (like EXIM etc) / Project Developers – entrepreneurs, which are not paid back as few of these projects are not functioning and still no action taken to recover the Capital Subsidy paid or Tax recovery which was availed through Accelerated Depreciation (AD).

If Government would have established all these projects from the Tax collections (which are doled out as free through AD), it would have needed only a fraction i.e only Rs. 51,504 Crores, which could have been managed from the taxes of Rs.137,344 Crores while retaining the land and property in Government’s name and could have generated lot of employment.

But, by giving an opportunity to Private sector, many have failed to deliver and no Action to recover the Capital Subsidy or the Debt (due to Tribunals etc…. Please be informed that Indian Parliament had to pass an act in Dec 2012 to recover debt (through wrong business cases of Project Promoters, approved by many banks which were certified by National and International Advisors or Consultants) which is around a whopping 40 Billion USD!!)

Total estimated Renewable energy project capacity = 12% of total installed 220GW = 26000 MW
Cost/ MW Investment Equity Debt Cap Sub AD
Source MW installed Total 30% 70% Rs(Cr) 80%adj
Biomass 6 4,500 27,000 8,100 18,900 6,750 21,600

Wind 7 20,160 131,040 39,312 91,728 104,832

Solar PV 10 1,300 13,000 3,900 9,100 VGF? 10,400
(Ground)